Choosing White Coated Board in 2026 requires more than comparing brightness, price, and surface gloss. The right grade must perform on press, during converting, and inside real distribution systems. A carton may look excellent under showroom lighting, yet crack sharply along its fold lines. That detail matters.
Recent industry research supports a careful approach. Smithers’ paperboard packaging studies highlight continued demand for printable, lightweight, and recyclable substrates. CEPI’s annual industry statistics also show how energy costs, fibre availability, and production changes influence European paper and board supply. These reports do not provide one universal specification. They show why buyers should verify current mill data instead of relying on old samples.
“Paper packaging is renewable, recyclable and biodegradable,” says Jori Ringman, Director General of Cepi. His statement reflects the sector’s direction, but it should not end the discussion. Recyclability depends on coatings, inks, barriers, recycling systems, and local acceptance rules. The label alone is insufficient.
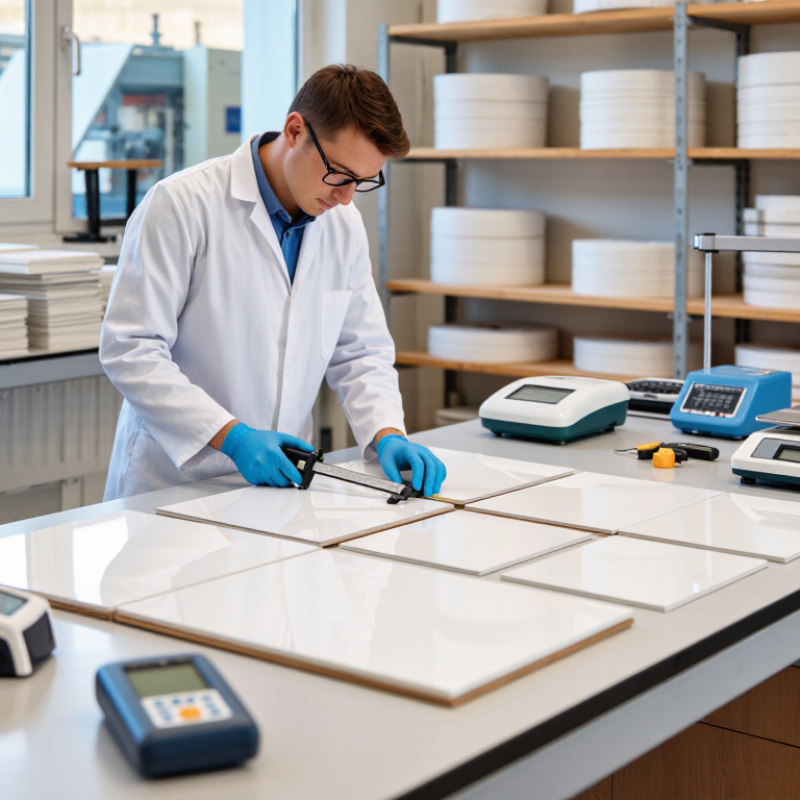
Measure the board before approving it. Check grammage, caliper, stiffness, brightness, opacity, surface strength, Cobb value, and folding performance. Ask for technical data sheets, food-contact declarations where relevant, chain-of-custody evidence, and recent batch samples. Test the board with your actual ink, varnish, die, and folding equipment.
No grade is perfect.
A heavier sheet may improve rigidity but increase material use and shipping weight. A highly bright surface may improve image contrast but cost more. This guide examines those trade-offs, including several assumptions buyers should question before placing a 2026 order.
How to Choose White Coated Board in 2026?
What Is White Coated Board and How Is It Made?
White coated board is a stiff, multi-layer paperboard with a smooth, bright surface. It usually contains bleached or recycled fibers, mineral fillers, starch, and coating pigments. Kaolin and calcium carbonate improve whiteness and print detail. Water-based binders help the coating stay attached.
Manufacturing begins with fiber preparation and sheet forming. Several plies are pressed together, then dried. A coating machine applies one or more thin layers. Calendering compresses the surface and controls gloss. The finished board may be coated on one or both sides. FAOSTAT reported global paper and paperboard production at roughly 417 million tonnes in 2022. That scale shows why fiber selection and recovery matter. Yet, a brighter sheet is not automatically better. Excess coating can reduce recyclability and weaken folding performance.
Tips: Check grammage, caliper, stiffness, moisture resistance, and surface strength. Match the board with offset, flexographic, or digital printing. Inspect the cut edge for loose fibers. Fold a sample across and along the grain. In practical converting tests, a board can print beautifully but crack at the crease. Food packaging also requires documented compliance with applicable contact-material rules. Ask for certificates, recycled-fiber details, and test results from the supplier. Recheck them after changing the coating or production batch.
White coated board is a paperboard substrate covered with one or more layers of mineral pigments and binders. The coating improves whiteness, smoothness, printability, and surface protection. Choose the grammage according to the required stiffness, folding performance, printing quality, and end use.
How it is made: Cellulose fibers are mixed with water, formed into a sheet, pressed, and dried. A white pigment coating, commonly based on mineral materials such as calcium carbonate or kaolin, is then applied and dried. Calendering smooths the surface before the board is cut and finished for printing or converting.
The chart shows typical industry grammage ranges by application. Actual specifications vary according to fiber composition, board structure, coating design, moisture, and required stiffness.
Choosing white coated board in 2026 starts with identifying its construction, not its whiteness. Solid bleached sulfate board uses virgin fibers and offers a clean reverse side, high stiffness, and sharp print reproduction. Folding boxboard usually combines multiple layers, often with a mechanical-fiber middle layer. It can reduce weight while maintaining folding performance. White-lined chipboard, also called recycled coated board, uses recovered fibers. Its surface prints well, but the reverse side may look gray and its stiffness can vary.
The differences are visible on a sample sheet. SBS feels dense and smooth. FBB bends cleanly without cracking. Recycled board may show tiny surface specks under strong light. There is no perfect type. Sometimes, I overvalue brightness and overlook package rigidity. That is a costly mistake.
Smithers’ 2024 packaging research identifies folding cartons as a major paperboard packaging segment, supported by food, pharmaceutical, and household demand. CEPI reported approximately 79 million tonnes of European paper and board production in 2023, reinforcing the scale of fiber-based packaging. The Confederation of European Paper Industries also reports that recycled fiber remains central to Europe’s circular material system. Choose SBS for premium graphics and demanding surfaces. Choose FBB when stiffness and lower basis weight matter. Choose recycled coated board when recovered content and cost deserve priority. Confirm caliper, moisture resistance, coating adhesion, and food-contact compliance before purchasing. Supplier data can be incomplete. Test the actual converting line.
The table below compares common white coated board categories. Basis weights, brightness, and performance are typical industry ranges; exact specifications vary by mill, fiber mix, coating formulation, and finishing process.
| Board Type | Typical Fiber Structure | Coating Sides | Typical Basis Weight | Typical ISO Brightness | Main Advantages | Common Applications | Key Selection Considerations |
|---|---|---|---|---|---|---|---|
| Solid Bleached Sulfate (SBS) | Primarily bleached chemical pulp throughout the sheet; usually a clean white reverse side. | Usually coated on one or both sides; commonly C1S or C2S. | 180–600 gsm | 88–95% | Excellent printability, smoothness, whiteness, die-cutting, folding, and premium appearance. | Premium folding cartons, cosmetics packaging, pharmaceuticals, confectionery, luxury retail packaging, and graphic covers. | Choose when high visual quality, accurate color reproduction, and a white reverse side are important. Check moisture resistance and food-contact compliance where required. |
| Folding Boxboard (FBB) | Multi-ply board with bleached chemical-pulp outer layers and a mechanical-pulp or high-yield middle layer. | Typically coated on the printing side; some grades are coated on both sides. | 170– hacía 500 gsm | 80–92% | High stiffness at relatively low weight, good folding performance, bright print surface, and efficient material usage. | Food cartons, personal-care packaging, household products, pharmaceutical cartons, and general folding boxes. | A strong general-purpose choice when stiffness-to-weight ratio and folding quality matter. Confirm the reverse-side appearance and internal ply structure. |
| White-Lined Chipboard (WLC) | Recovered paper or recycled fiber in the middle and back layers, with a white coated top layer. | Generally coated on one side; reverse side is usually gray or off-white. | 250–700 gsm | 70–88% | Cost-effective, available in heavier weights, and suitable for many standard packaging formats. | Secondary packaging, dry-food cartons, consumer-product boxes, promotional packaging, and general retail cartons. | Choose for cost control and recycled-content objectives. Check odor, cleanliness, stiffness, moisture resistance, and suitability for direct food contact. |
| Coated Kraft Back Board | Strong kraft-based or mixed-fiber core with a white coated printing surface; the reverse side may be brown or cream. | Usually one-side coated. | 250–600 gsm | 75–90% | Good tear resistance, structural strength, and a contrast between a white print face and kraft-style reverse. | Takeaway packaging, bakery boxes, food-service cartons, carrier packaging, and packages requiring extra strength. | Select when durability and a natural or kraft appearance are useful. Verify grease resistance, odor requirements, and printing behavior on the reverse side. |
| C1S White Coated Board | A broad product format that may use virgin fiber, recycled fiber, or a multi-ply construction. | Coated on one side only. | 180–600 gsm | 78–93% | Good front-side print quality with lower material and coating cost than two-side-coated board. | Labels, cards, sleeves, folding cartons, tags, book covers, and packaging with an unprinted reverse. | Use when only one side needs a premium print surface. Confirm reverse-side color, caliper, folding direction, and surface strength. |
| C2S White Coated Board | May be made from bleached virgin pulp, recycled fiber, or a multi-ply combination depending on the grade. | Coated on both sides. | 180–500 gsm | 80–95% | Consistent two-sided appearance, strong image reproduction, and suitability for premium printed pieces. | Premium cards, brochures, display cards, book covers, two-sided packaging, and high-quality promotional materials. | Choose when both sides require smoothness and consistent color. Compare stiffness, caliper, folding crack resistance, and finishing compatibility. |
| Barrier-Coated White Board | Base board can be virgin-fiber or recycled; an additional coating or dispersion layer provides functional resistance. | Usually one-side coated, with optional functional coating on the reverse or inner surface. | 200–600 gsm | 75–94% | Improved resistance to moisture, grease, oil, aroma, or mineral-oil migration, depending on the coating system. | Food-service packaging, frozen-food cartons, bakery packaging, cups, trays, and products exposed to humidity or grease. | Specify the exact barrier requirement rather than relying on the term “barrier board.” Check heat-sealing, recyclability, repulpability, food-contact rules, and end-use temperature. |
Note: GSM, brightness, stiffness, coating performance, and barrier properties are indicative ranges rather than universal specifications. Always approve a technical data sheet and production sample before finalizing the grade.
Choosing white coated board in 2026 means matching specifications to the project, not chasing the highest brightness. Smithers’ 2024 folding-carton market analysis valued global demand at roughly US$100 billion in 2023. That scale increases pressure for consistent printing, lighter structures, and reliable converting performance. Start with the finished pack. A cosmetic carton needs smoothness and sharp color, while a shipping sleeve needs stiffness and compression strength.
Specify grammage and caliper together. A 300 gsm board may perform differently from another 300 gsm grade. ISO 536 supports grammage testing, while ISO 534 measures thickness. Use these values to estimate bulk and stiffness before approving artwork. In my production experience, excessive caliper can improve shelf presence but create cracking on tight folds. It can also reduce the number of sheets per pallet. Small details matter.
Match coating to the printing process. Gloss coating can strengthen image contrast, but matte surfaces often reduce glare during retail inspection. For offset printing, request data aligned with ISO 12647-2, including brightness, whiteness, ink absorption, and surface strength. Ask for Cobb water absorption results when humidity or chilled products are involved. The awkward part is that laboratory results may not predict every folding failure. I would run a short press trial, inspect crease lines, and test filled cartons under realistic storage conditions. Do not approve from samples alone.
Printability starts with surface consistency, not brightness alone. ISO 12647-2 recommends process control through measured color values and tolerance checks. Ask for laboratory data, including whiteness, gloss, roughness, and ink absorption. A board with excessive absorption can produce dull reds and fuzzy small text. High gloss may sharpen images, but it can also increase glare under store lighting.
Durability needs practical testing. Measure stiffness in both machine and cross directions. Check Cobb60 water absorption under TAPPI T 441, especially for chilled or humid environments. A lower Cobb value usually indicates better resistance to short water exposure. Still, it does not guarantee moisture-proof packaging. Crease cracking often appears after folding, not during a flat-sheet inspection. Test printed samples after creasing, stacking, and rubbing. Small details matter.
Surface quality should remain stable across the roll or sheet stack. Smithers’ 2024 folding-carton market analysis identifies premium graphics and efficient converting as continuing demand drivers. That makes coating uniformity commercially important. Request several production samples, not one perfect sheet. Compare ink density, pinholes, curl, and edge damage under identical lighting. My own mistake was trusting a bright sample before testing fine text. It looked excellent, but heavy ink areas dried slowly. A second trial exposed the weakness. Choose the board that performs consistently, even when the test conditions are less forgiving.
Supplier comparison should begin with measurable specifications, not attractive samples. Check basis weight, thickness, coating uniformity, brightness, moisture, and sheet flatness. Request samples from the same grade and test them on your own press. A board that looks excellent under showroom lighting may crack during folding. Ask for recent quality records, production capacity, minimum order quantities, and realistic lead times. Also confirm how the supplier handles damaged pallets and inconsistent batches.
Supplier comparison
Check measurable specifications, production reliability, and quality consistency before making a decision.
Cost comparison must include more than the quoted price per ton. Add freight, import charges, storage, trimming loss, printing adjustments, and rejected sheets. A cheaper board can become expensive after slow drying or poor runnability. Ask suppliers to provide a landed-cost estimate with clear assumptions. I have learned that verbal promises are difficult to verify. Written specifications and retained samples are safer.
Tips:
Compare at least three suppliers using one score sheet. Record price, delivery, defect rate, coating performance, and payment terms.
For sustainability, request recycled-fiber content, responsible-forestry certification, mill energy data, water-use information, and recyclable packaging details. Do not accept vague “eco-friendly” claims without supporting documents. A lower-carbon option may still require more transport or create higher waste. That trade-off deserves honest review. My own evaluation is never perfect, especially when supplier data uses different boundaries. Recheck the figures before making a long-term decision.
©2024 Pine Vista LLC, DBA Design Manufacturing Group. All Rights Reserved.


©2024 Pine Vista LLC, DBA Design Manufacturing Group. All Rights Reserved.
